
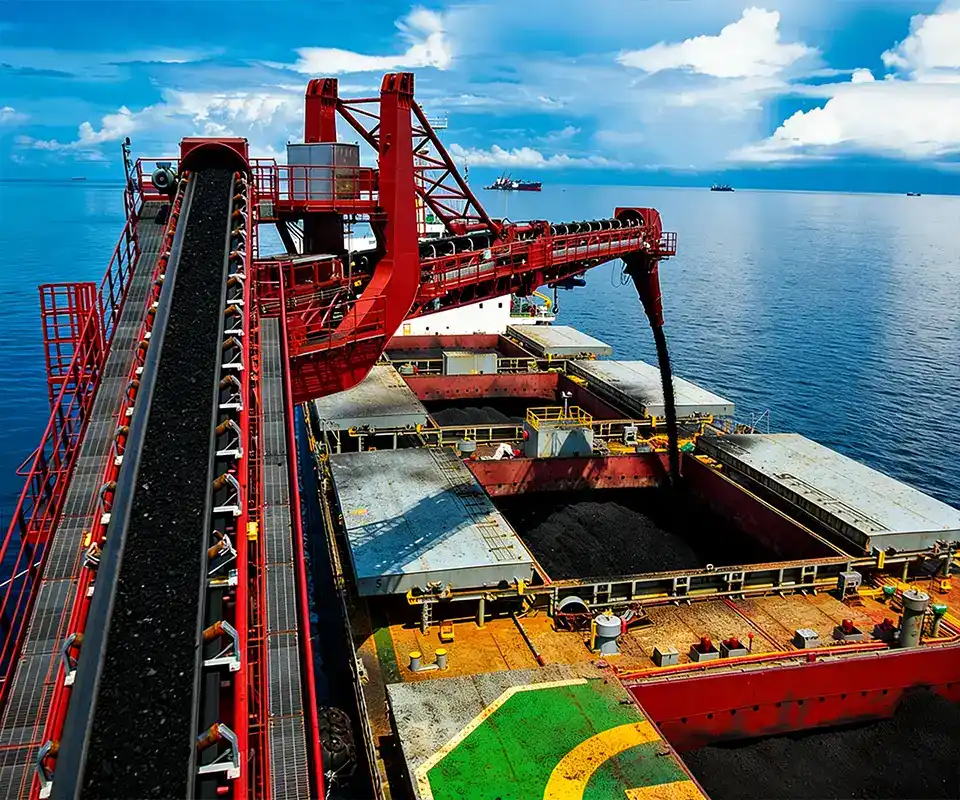
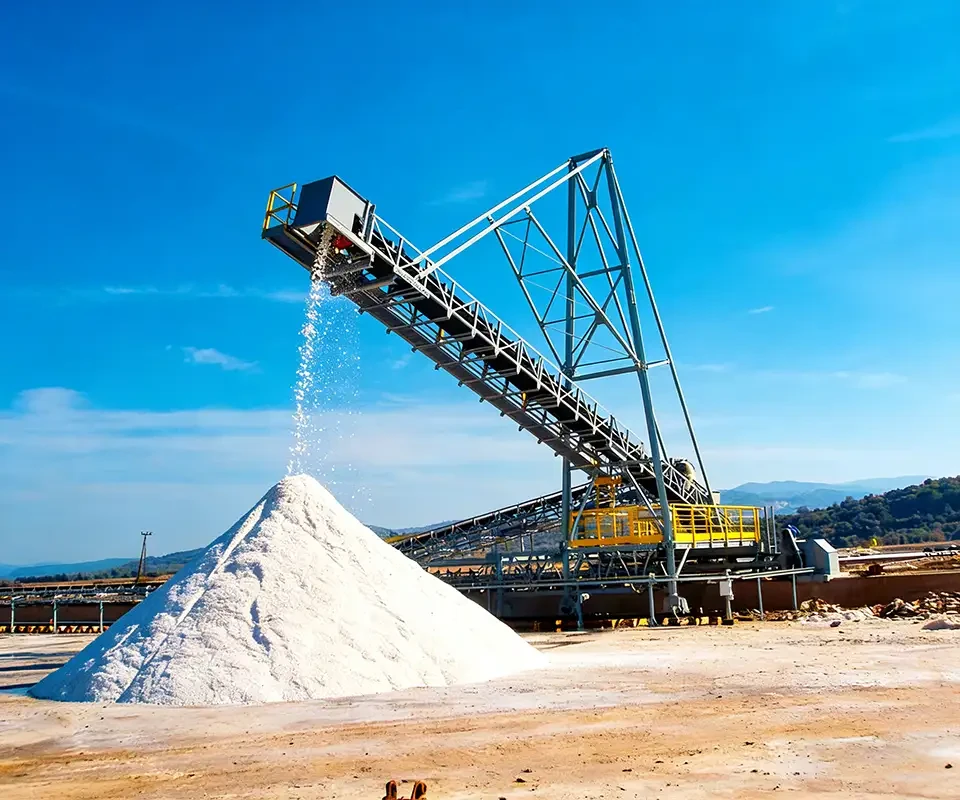
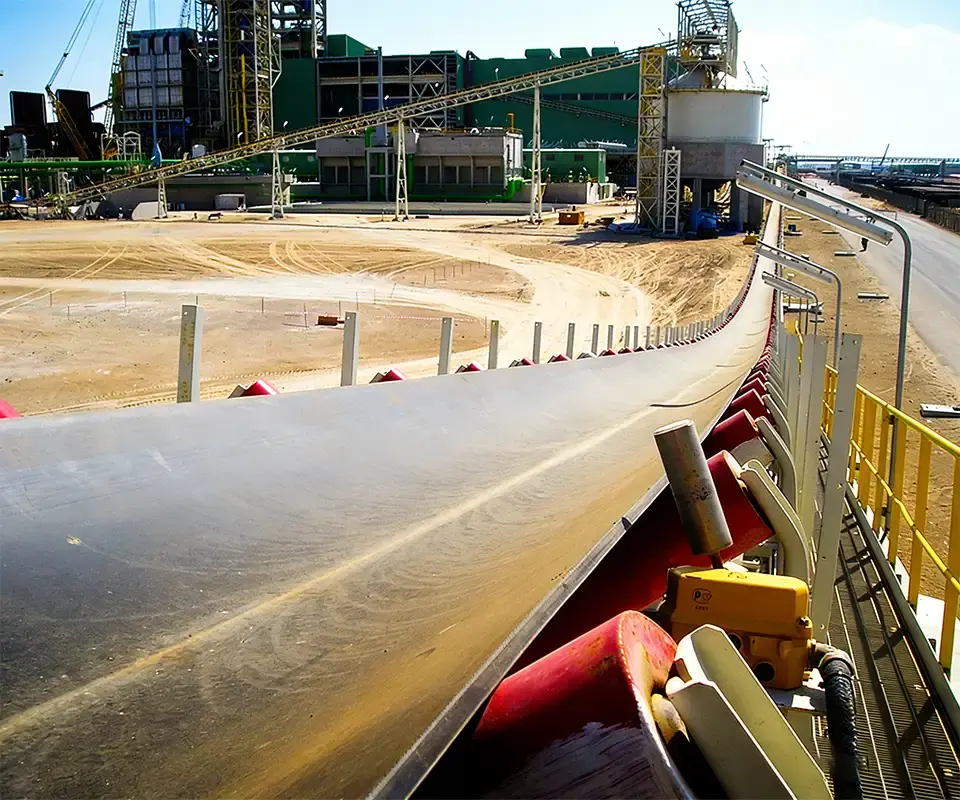
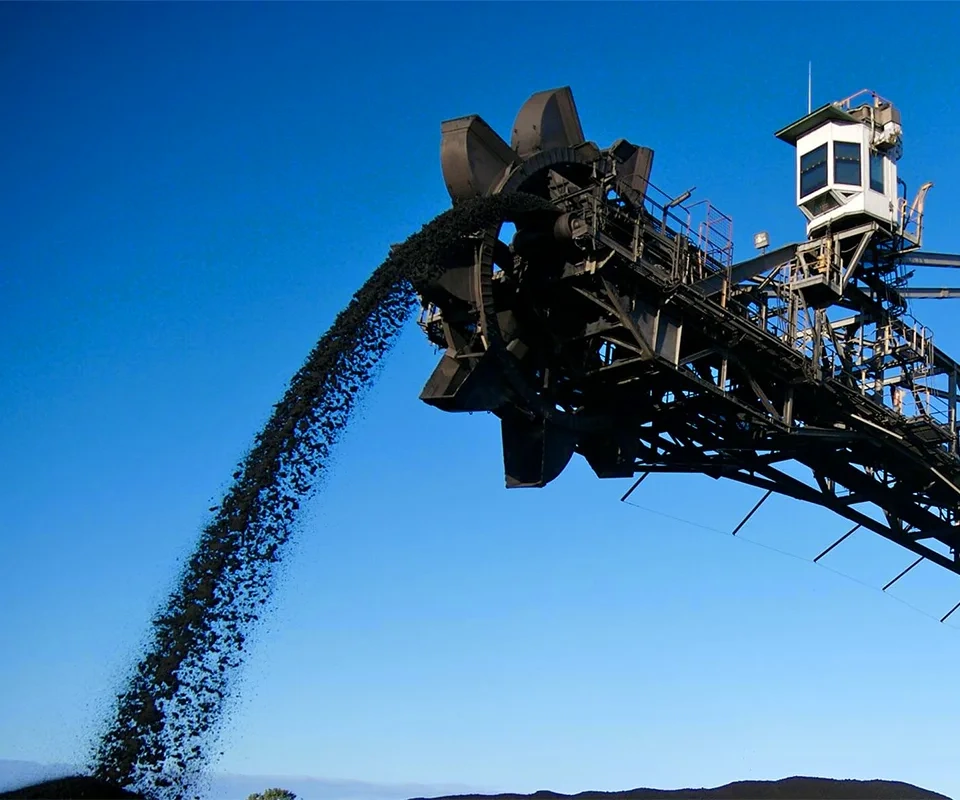
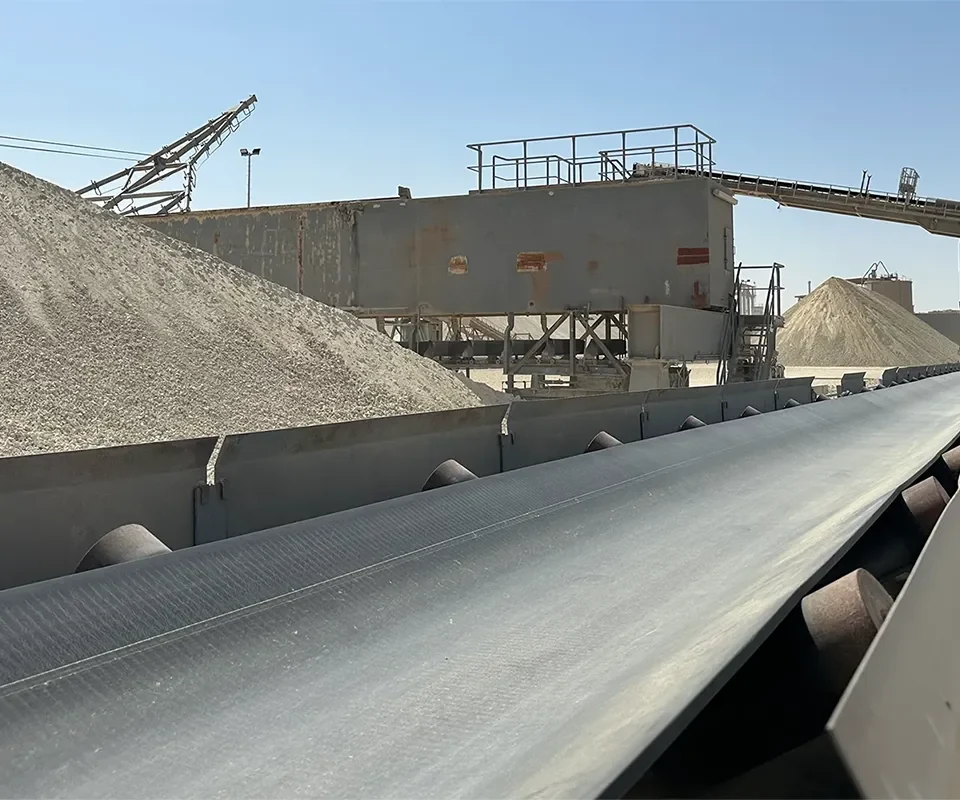
Australia operates some of the world’s most demanding mining conveyor systems. Iron ore operations in the Pilbara, coal mines in Queensland and New South Wales, gold and lithium projects in Western Australia, hard-rock mines, mineral processing plants, and export terminals all rely on conveyor belts to move large volumes of material safely and continuously.
According to Geoscience Australia, the country was a top-five global supplier of 14 mineral commodities in 2024. This scale of production creates strong demand for steel cord conveyor belts, fabric-reinforced belts, flame-resistant belts, abrasion-resistant belts, heat-resistant belts, and specialist products designed for long-distance and high-capacity conveying.
Choosing a mining conveyor belt supplier in Australia is therefore not simply a matter of comparing prices per metre. Belt failure can interrupt an entire production chain, delay vessel loading, reduce crusher utilisation, or force an unplanned shutdown. Buyers must evaluate belt construction, engineering support, local service capability, safety compliance, delivery reliability, splicing support, monitoring technology, and total cost per tonne conveyed.
This article reviews four established suppliers serving Australian mining operations and introduces SHENGYUAN as the fifth option for planned procurement, custom specifications, factory-direct coordination, and consolidated sourcing of conveyor belts and related components. The order is a practical industry shortlist based on publicly available product information, mining relevance, service capability, and market presence. It is not an official market-share ranking.
Quick answer: Five notable mining conveyor belt suppliers serving Australia are Fenner Conveyors, Continental Australia, REMA TIP TOP Australia, All Rubber, and SHENGYUAN. Local suppliers offer strong installation and emergency service capabilities, while SHENGYUAN provides an attractive factory-direct option for planned bulk orders, custom belt specifications, and integrated conveyor component procurement.
Why Mining Conveyor Belt Selection Matters in Australia
Australian mining conveyors frequently operate under high tension, heavy loading, abrasive material contact, intense sunlight, dust, moisture, and large temperature variations. Many systems are located far from major cities, which makes emergency replacement more expensive and logistically difficult.
A conveyor belt used for iron ore in Western Australia may need high tensile strength, excellent abrasion resistance, and reliable splice performance over a long route. A belt used in an underground coal mine may require flame-resistant and antistatic properties. A gold processing plant may need resistance to impact, moisture, and sharp crushed material. Port conveyors may require high-capacity operation and protection from coastal conditions.
The correct supplier should therefore ask about the conveyed material, lump size, bulk density, belt speed, conveyor length, vertical lift, operating tension, loading impact, pulley diameter, temperature, moisture, and safety requirements before recommending a belt.
Australian procurement priority: Mining customers generally value direct communication, realistic delivery commitments, traceable quality records, safety documentation, and evidence that a product is suitable for the stated operating duty. An inexpensive belt without reliable technical support can create a much higher life-cycle cost.
How to Evaluate a Mining Conveyor Belt Supplier
| Evaluation Area | What Buyers Should Confirm |
| Product Range | Fabric, steel cord, solid woven, abrasion-resistant, heat-resistant, flame-resistant, sidewall, and special belts. |
| Technical Selection | Belt strength, cover grade, cover thickness, carcass type, splice method, minimum pulley diameter, and safety factor. |
| Quality and Standards | Relevant ISO, DIN, Australian Standard, mine approval, fire resistance, antistatic, abrasion, adhesion, and tensile test documentation. |
| Service Capability | Installation, splicing, inspection, repair, condition monitoring, shutdown support, and emergency response. |
| Commercial Value | Purchase price, expected service life, freight, inventory requirements, downtime exposure, and cost per tonne conveyed. |
For underground coal applications, buyers should also confirm applicable fire-resistant and antistatic requirements, including mine approval conditions and standards such as AS 4606 where relevant. Textile-reinforced belting may be evaluated against standards such as AS 1332, while many international mining projects also use DIN or ISO-based specifications.
1. Fenner Conveyors
Fenner Conveyors, a Michelin Group company, is one of Australia’s most established mining conveyor belt manufacturers and service providers. The company designs, manufactures, installs, and services complete conveyor systems, giving it a broader capability than a supplier focused only on replacement belting.
Its belt range covers steel cord, fabric, solid woven, and application-specific products for surface and underground mining. Fenner also manufactures Australian-approved solid woven belts for underground applications and supports customers with belt installation, splicing, inspections, monitoring, maintenance, and system engineering.
Fenner has continued investing in Australian manufacturing. The addition of another production line increased its mining conveyor belt production capacity by approximately 40%, demonstrating a strong commitment to local supply and long-term mining demand.
A major advantage is its nationwide network. Service centres in Western Australia, Queensland, New South Wales, South Australia, Tasmania, and the Northern Territory help support planned shutdowns and urgent belt work near important mining regions.
Best suited for: Large Australian mines seeking locally manufactured belting, complete conveyor engineering, installation, splicing, monitoring, and long-term service support.
2. Continental Australia
Continental is a global conveyor belt manufacturer with local manufacturing and service capability in Australia. Its Australian operation produces steel cord and textile conveyor belting and supports mining, ports, infrastructure, agriculture, and industrial applications.
The Continental portfolio includes steel cord belts, textile belts, solid woven belts, steep-incline belts, enclosed conveying solutions, monitoring systems, installation services, and belt repair support. This range allows the company to serve short plant conveyors as well as long overland systems carrying high volumes of ore or coal.
Its Flexsteel range is designed for demanding mining conditions and includes strength ratings up to 4500 N/mm. High-strength steel cord belts can be valuable for long-distance conveyors because they provide high tensile capacity and relatively low elongation, helping maintain stable tension over extended routes.
Continental also provides digital monitoring technologies that can measure material flow, belt position, and operating conditions. Monitoring does not remove the need for inspections, but it can help maintenance teams identify developing problems before they become major failures.
Best suited for: Long-distance, high-tension, and high-capacity conveyors requiring steel cord technology, local manufacturing, field services, and advanced belt monitoring.
3. REMA TIP TOP Australia
REMA TIP TOP Australia supplies conveyor belting and provides installation, splicing, maintenance, wear protection, surface protection, and bulk material handling services. Its conveyor belt portfolio includes fabric-ply, steel cord, and solid woven constructions suitable for mining, quarrying, construction, and industrial processing.
The company has more than 30 years of experience in conveyor belting and supports mining customers through regional workshops and service teams. Its capabilities extend beyond product supply to conveyor inspections, audits, shutdown maintenance, installation management, mechanical maintenance, and repair materials.
This service-led model is particularly valuable in the Pilbara and other remote mining regions. A belt may be correctly specified but still fail early because of poor installation, incorrect splicing, mistracking, seized rollers, excessive impact, or ineffective cleaning. A supplier with field service capability can investigate the complete conveyor rather than only replacing the damaged belt.
REMA TIP TOP has also secured multi-site conveyor maintenance work for major Western Australian iron ore operations, indicating experience with large mining customers and demanding safety and operational requirements.
Best suited for: Mines requiring conveyor belting together with professional splicing, shutdown maintenance, inspections, wear protection, and site-based service teams.
4. All Rubber
All Rubber is a Western Australian conveyor belting and rubber technology supplier with more than 50 years of industry experience. The company serves mining, cement, power generation, manufacturing, ports, terminals, recycling, and other bulk material handling industries.
Its conveyor belt range includes fabric belts, steel cord belts, fire-resistant and antistatic products, oil-resistant belts, heat-resistant belts, and application-specific constructions. The company also provides conveyor accessories, rubber lining, belt fasteners, pulley lagging, maintenance products, and custom solutions.
All Rubber supplies fabric belts in multiple ply constructions, with stocked widths from approximately 350 mm to 2400 mm without longitudinal joints. Heavy-ply designs are available for demanding mining and material processing duties, while wider or customized products can be considered for special applications.
Its Western Australian location is commercially useful for mining and processing customers that value accessible technical communication, local stock, and practical support. It can be a strong option for replacement belts, maintenance supplies, and projects requiring both belting and rubber protection products.
Best suited for: Western Australian mines, quarries, cement plants, and industrial operators seeking conveyor belts, rubber lining, accessories, and locally supported custom solutions.
5. SHENGYUAN: A Factory-Direct Supply Option
Australian suppliers offer important advantages for emergency replacement, site inspection, belt installation, splicing, and local maintenance. However, not every order is urgent. Mines, EPC contractors, distributors, and conveyor service companies often plan belt replacement months before a shutdown. For these planned orders, an international factory-direct supply partner can offer meaningful commercial benefits.
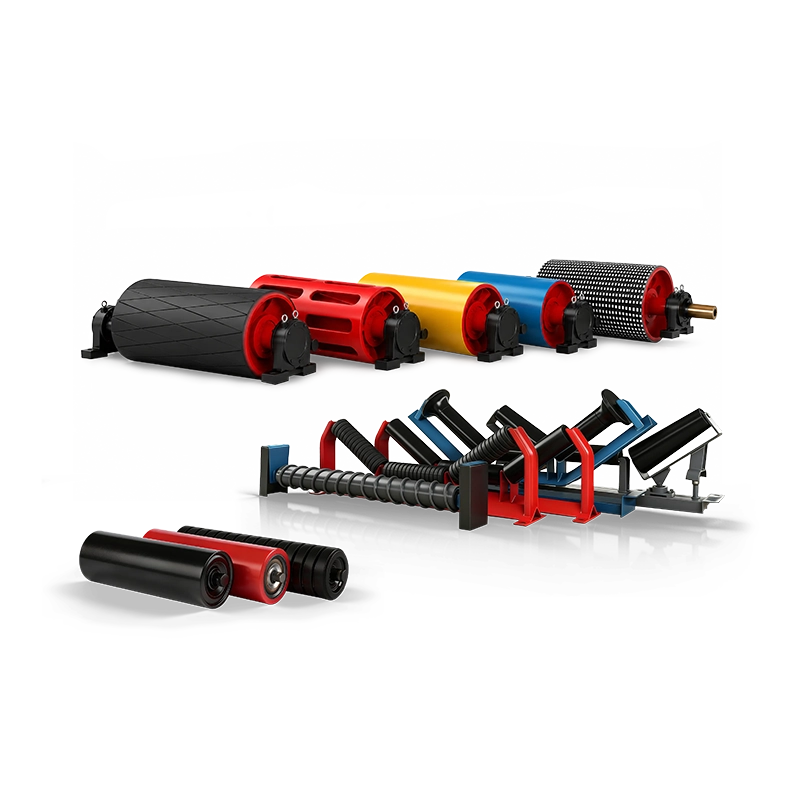
SHENGYUAN, the brand of Hebei Shengwen Mining Machinery Co., Ltd., has nearly two decades of experience in heavy-duty bulk material conveying equipment. The company supplies conveyor belts together with conveyor rollers, pulleys, idlers, cleaners, and related components for mining, coal, cement, aggregates, ports, power plants, and industrial handling systems.
Its heavy-duty conveyor belt range includes rubber fabric belts, EP belts, NN belts, steel cord belts, abrasion-resistant belts, heat-resistant belts, flame-resistant belts, chevron belts, sidewall belts, endless belts, pipe conveyor belts, and PVC or PVG solid woven products.
Why Australian Buyers May Consider SHENGYUAN
Factory-Direct Cost Control
Direct technical and commercial communication can reduce unnecessary trading layers and support competitive pricing for planned and volume orders.
Application-Based Selection
Belts can be selected according to material, tension, capacity, length, incline, temperature, abrasion, safety requirements, and maintenance conditions.
Consolidated Component Supply
Customers can combine belts, rollers, pulleys, idler frames, and belt cleaners in one coordinated procurement package.
Through its custom conveyor solutions, SHENGYUAN can review customer drawings and technical requirements before confirming a proposal. Selection may include belt width, tensile rating, carcass material, number of plies, top and bottom cover thickness, rubber grade, edge construction, roll length, fire resistance, temperature resistance, and special surface profiles.
An additional advantage is integrated system compatibility. Conveyor belt performance is affected by rollers, pulley diameters, lagging, loading zones, take-up tension, tracking, and cleaners. Buyers sourcing several components together can review these relationships before production instead of treating each item as an unrelated purchase.
For Australian customers, SHENGYUAN is best suited to scheduled procurement rather than emergency replacement. A mine can order belts and spare conveyor components before a planned shutdown. A distributor can develop local inventory. An EPC contractor can source non-standard products according to drawings. A service company can consolidate multiple belt, roller, and pulley requirements into one shipment.
The company’s service and logistics support includes order communication, production coordination, reinforced export packaging, shipment planning, and after-sales assistance for international projects.
Why choose SHENGYUAN?
SHENGYUAN is an attractive option for Australian buyers who can plan procurement in advance and need customized belt specifications, factory-direct pricing, coordinated component supply, English technical communication, and export-ready logistics. Its strongest applications include distributor inventory, EPC projects, OEM supply, annual replacement programmes, and multi-component mining conveyor packages.
Supplier Comparison at a Glance
| Supplier | Primary Strength | Suitable Purchasing Situation |
| Fenner Conveyors | Australian manufacturing and complete conveyor life-cycle support | Major mines needing local products, installation, and service |
| Continental Australia | Steel cord technology, monitoring, and field services | Long-distance and high-tension mining conveyors |
| REMA TIP TOP Australia | Belting, splicing, maintenance, and site services | Mines requiring shutdown and field maintenance support |
| All Rubber | Local belting, rubber lining, and accessories | Western Australian mining and industrial replacement needs |
| SHENGYUAN | Factory-direct customization and integrated component sourcing | Planned orders, distributors, EPC projects, OEM supply, and bulk procurement |
Local Supplier or International Factory?
For an urgent belt failure, a local Australian supplier normally provides the lower-risk solution. Local teams can inspect the conveyor, arrange equipment, splice the belt, manage site procedures, and respond during a shutdown. These services are difficult to replace through international supply alone.
For planned purchasing, the commercial calculation changes. An international factory-direct supplier may provide attractive pricing, broader customization, and consolidated shipments when lead time is properly managed. The buyer should include production time, sea freight, customs clearance, local transport, inspection, installation, and contingency stock in the procurement schedule.
A practical strategy is dual sourcing. Local companies can support inspections, installation, emergency work, and immediate maintenance. SHENGYUAN can support planned replacement belts, customized products, distributor inventory, and packages containing conveyor belts, rollers, pulleys, and idler assemblies.
Conclusion: Select a Supplier Based on Operating Risk
Fenner Conveyors, Continental Australia, REMA TIP TOP Australia, and All Rubber offer established products and services for Australian mining operations. Fenner is strong in local manufacturing and complete conveyor support. Continental provides advanced steel cord belts and monitoring technology. REMA TIP TOP combines belting with extensive field maintenance. All Rubber offers practical Western Australian supply and rubber technology experience.
SHENGYUAN provides a different purchasing model. Its value lies in factory-direct coordination, custom belt selection, integrated conveyor component sourcing, and export support. This makes it a persuasive alternative for buyers who can plan ahead and want to control procurement cost without limiting customization.
The best supplier is not necessarily the nearest company, the largest brand, or the lowest quotation. The correct decision depends on belt duty, safety requirements, service urgency, technical complexity, order volume, delivery schedule, and total cost of ownership. Buyers should request a technically complete proposal and compare expected performance rather than price alone.
Planning a mining conveyor belt order for Australia?
Provide SHENGYUAN with the material type, bulk density, lump size, belt width, belt speed, conveyor length, vertical lift, required capacity, tensile rating, cover thickness, operating temperature, safety requirements, pulley data, quantity, and expected delivery date. The technical team can review the application and prepare a customized belt and conveyor component proposal.