
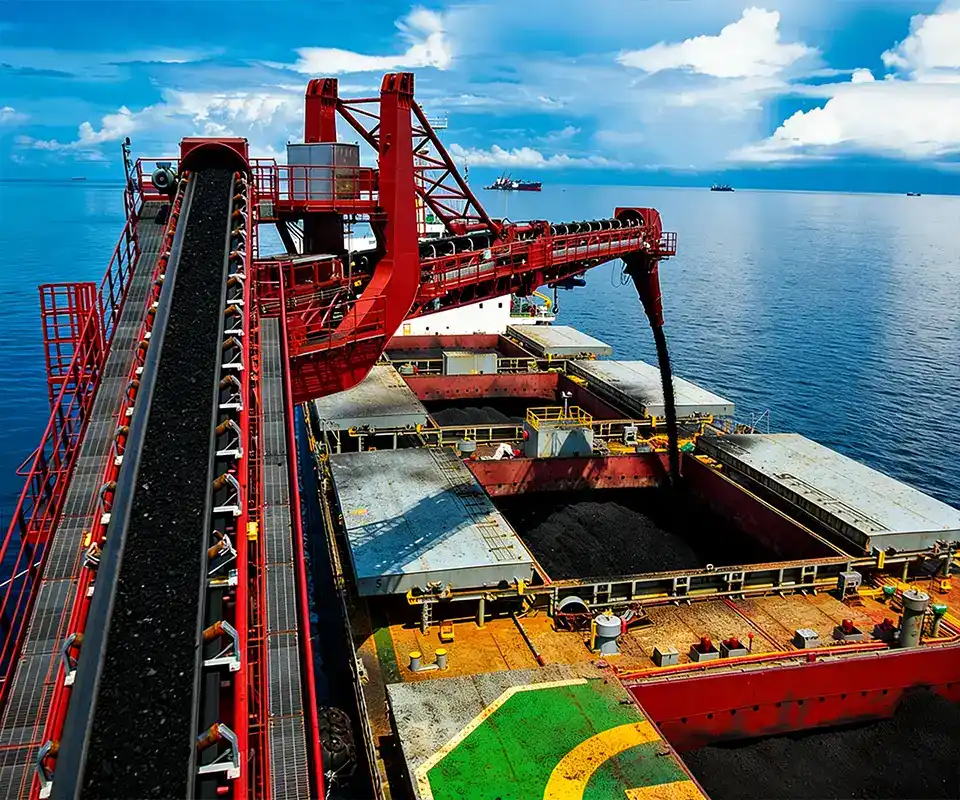
Selecting low-resistance idlers for long mine conveyors is an important part of reducing conveyor operating costs, improving energy efficiency, and maintaining reliable bulk-material transportation. In mining operations, long-distance belt conveyors may extend several kilometres and use thousands of carrying and return rollers. Although the resistance of one roller may appear small, the combined effect of thousands of rollers operating continuously can become significant.
For iron ore, copper, coal, limestone, and other heavy-duty mining conveyors, energy efficiency depends on more than the motor and gearbox. Conveyor idler bearings, seals, roller diameter, shell construction, alignment, and operating load can all influence the resistance that the drive system must overcome.
However, an idler described as low resistance is not automatically suitable for a long mine conveyor. A roller that spins freely without a load may perform differently when exposed to heavy radial loading, belt speed, dust, moisture, low temperatures, and continuous operation.
Furthermore, roller rotational resistance is only one contributor to conveyor energy consumption. The deformation of the conveyor belt cover as it passes over the rollers can also create substantial resistance. Selecting an efficient idler therefore requires an understanding of both the roller and the complete belt-support system.
The correct selection should consider measured rotational resistance, bearing friction, seal drag, roller diameter, operating load, belt speed, temperature, idler spacing, manufacturing accuracy, durability, and total lifecycle cost.
Quick answer: Choose low-resistance idlers for long mine conveyors using verified rotational resistance under representative loads, speeds, and temperatures. Compare bearing design, seal construction, lubrication, roller diameter, shell and shaft strength, and manufacturing tolerances. Evaluate carrying and return rollers separately, and calculate the potential energy savings across the complete conveyor. A low hand-spinning resistance or a lightweight roller shell alone does not prove lower operating power. The best selection balances energy savings with bearing life, contamination protection, mechanical reliability, and purchase cost.
Why Low-Resistance Idlers Matter on Long Mine Conveyors
A short belt conveyor may contain only a limited number of idler sets, making the energy contribution of each roller relatively small compared with the total power requirement.
A long overland mining conveyor can contain many thousands of individual rollers. Each roller must rotate as the belt moves, overcoming resistance from bearings, seals, lubrication, and other mechanical effects.
Even a modest reduction in average rotational resistance can become valuable when multiplied across the installed roller population and the conveyor’s annual operating hours.
Low-resistance idlers can offer several potential benefits:
- Lower mechanical resistance along the carrying and return strands.
- Reduced drive power requirements under comparable operating conditions.
- Potential reductions in annual electrical energy consumption.
- Reduced resistance-related mechanical losses when properly engineered.
- Improved lifecycle economics where energy savings exceed additional costs.
- Opportunities to optimize roller diameter, spacing, and bearing design.
However, these benefits should be demonstrated through suitable testing and conveyor calculations. Not every conveyor experiences the same proportion of energy loss from idler rotational resistance.
1. Understand the Different Sources of Conveyor Resistance
One of the most important technical distinctions is the difference between idler rotational resistance and conveyor belt indentation rolling resistance.
Although both contribute to the energy needed to operate a conveyor, they arise from different physical mechanisms and should not be treated as the same performance characteristic.
Idler Rotational Resistance
Idler rotational resistance is the mechanical resistance that must be overcome to rotate the roller around its shaft.
Its principal contributors include bearing friction, lubricant resistance, seal drag, and effects associated with the bearing arrangement and assembly condition.
Belt Indentation Rolling Resistance
Indentation rolling resistance occurs when the conveyor belt’s lower rubber cover is repeatedly deformed as it travels over the supporting idler rollers.
Because rubber exhibits viscoelastic behavior, energy is dissipated during the deformation and recovery process. The resulting resistance depends on belt cover properties, roller diameter, loading, temperature, and operating speed.
Other Conveyor Resistances
Additional losses may result from belt flexure, bulk material deformation, unintended sliding, misalignment, transfer points, and other conveyor components.
| Resistance Type | Main Cause | Possible Improvement |
| Idler Rotational Resistance | Bearings, seals, lubricant and assembly conditions | Optimized bearings, sealing, lubrication and roller diameter |
| Indentation Rolling Resistance | Viscoelastic deformation of the belt cover | Suitable belt bottom cover, roller diameter and loading arrangement |
| Belt Flexure Resistance | Repeated bending between supporting rollers | Appropriate belt construction, support geometry and spacing |
| Material Flexure Resistance | Deformation and movement of the conveyed material | Suitable loading, belt sag and conveyor geometry |
| Unintended Sliding Resistance | Misalignment or relative sliding at contact surfaces | Accurate installation and correction of belt tracking problems |
A low-resistance roller can reduce its own rotating losses, but it does not automatically eliminate indentation resistance or other conveyor losses.
Engineering principle: Rotational resistance is primarily a characteristic of the idler assembly, while indentation rolling resistance depends strongly on the interaction between the roller and the conveyor belt. Both should be assessed when optimizing energy consumption on a long mine conveyor.
2. How Is Idler Rotational Resistance Measured?
Idler rotational resistance may be expressed as a resisting torque or as an equivalent tangential resistance force at the roller circumference.
For a roller with a known effective radius, the relationship between resisting torque and equivalent tangential resistance force is:
Fr = Mr / r
Fr: Equivalent tangential rotational resistance (N); Mr: Resisting torque (N·m); r: Effective roller radius (m).
The value should be measured using a defined test method and appropriate operating conditions.
A controlled laboratory test may measure the torque needed to rotate the roller at a specified speed and under defined radial or axial loading. Other methods may use roller deceleration or specialized test rigs to estimate resistance.
Because test methods differ, resistance values from unrelated tests cannot always be compared directly.
For accurate purchasing decisions, request the measured value together with the test speed, applied load, temperature, measurement method, and test conditions.
3. Why a Hand-Spin Test Is Not Enough
A common way to compare rollers is to rotate them manually and observe which one spins for the longest time.
Although a hand-spin test can reveal some obvious problems, such as severe bearing damage or mechanical interference, it is not a reliable standalone measure of energy efficiency.
The result can be influenced by roller mass, rotational inertia, initial speed, bearing condition, seal drag, and the absence of representative operating load.
A heavy roller with substantial rotational inertia may continue spinning for a long time even if its loaded operating resistance is not particularly low.
Conversely, a roller with contact seals may stop relatively quickly during a manual test but provide better protection against contamination under demanding mine conditions.
The correct comparison requires controlled testing at representative operating speeds and loads.
Important: Free-spinning time is not equivalent to measured rotational resistance under load. Do not approve an energy-saving idler solely because it spins longer by hand than a competing roller.
4. Bearing Selection Has a Major Influence on Resistance
Bearings are a critical part of low-resistance conveyor idler design.
The bearing system must support the roller’s operating loads while maintaining smooth rotation, suitable lubrication, and an acceptable service life.
Bearing friction depends on several factors:
- Bearing type and internal geometry.
- Radial and axial load.
- Rotational speed.
- Internal clearance and fit.
- Lubricant type and viscosity.
- Manufacturing precision.
- Installation alignment and assembly quality.
- Operating temperature and contamination.
High-quality rolling bearings can provide low friction and reliable operation when selected for the actual load and environmental conditions.
However, bearing selection should not prioritize low resistance at the expense of adequate load capacity or service life.
An undersized bearing may offer low resistance under light laboratory conditions but perform poorly under heavy mine conveyor loading.
For long-distance conveyors, suppliers should specify bearing size, model, load rating, internal clearance, and the intended operating conditions.
5. Bearing Clearance Must Match the Application
Bearing internal clearance affects the way rolling elements operate under load and temperature.
Insufficient operating clearance can increase internal stresses and friction. Excessive clearance can create other problems involving load distribution, vibration, and bearing performance.
Research on conveyor idler bearing units has shown that bearing selection and internal clearance can influence measured rotational resistance under specific test conditions.
Nevertheless, a larger clearance class is not automatically the best choice for every low-resistance idler.
The required clearance depends on shaft and housing fits, temperature differences, bearing design, and the complete assembly.
The final selection should follow the bearing manufacturer’s engineering requirements and the expected operating conditions.
6. Seal Design: Low Drag vs Dust and Water Protection
Seal design is one of the most important trade-offs in low-resistance mining rollers.
A conveyor idler operates in environments that may contain fine mineral dust, abrasive particles, water, mud, and other contaminants. If these materials enter the bearing system, they can accelerate wear and increase friction.
Different sealing arrangements create different levels of drag and contamination protection.
Labyrinth Seals
Labyrinth seals use a series of closely controlled passages to restrict the movement of contaminants toward the bearing area.
Their resistance depends on the geometry, clearances, lubricant, and whether contact elements are incorporated into the sealing assembly.
Contact Seals
Contact seals use a sealing lip or another contact element to form a barrier against contamination. Depending on their construction, they may introduce additional friction because the sealing surface contacts a rotating component.
Combined Sealing Systems
Some heavy-duty rollers use multiple protective features, combining labyrinth geometry with additional seals or dust barriers.
The objective is to achieve suitable contamination protection without unnecessary rotational drag.
| Seal Consideration | Potential Benefit | Potential Concern |
| Non-Contact Labyrinth Geometry | Limited direct rubbing friction | Effectiveness depends on the complete seal and environment |
| Contact Lip Seal | Additional contamination barrier | May increase rotational resistance |
| Grease-Filled Seal Passages | Can contribute to contaminant exclusion | Viscous drag varies with grease and temperature |
| Multi-Stage Sealing Arrangement | Multiple protective barriers | Requires verification of total drag and protection |
An idler with exceptionally low initial drag but inadequate sealing may become less efficient as contaminants enter the bearing system. The energy cost of premature failure and replacement can outweigh the initial resistance advantage.
The best low-resistance seal is not necessarily the seal with the lowest measured friction. It is the sealing system that maintains acceptable resistance and protects the bearing throughout the intended service duty.
7. Lubrication Affects Resistance and Bearing Life
Lubrication is essential for reducing harmful metal-to-metal contact within rolling bearings and supporting reliable operation.
However, lubricant also contributes to resistance through viscous effects. The type, quantity, consistency, and temperature-dependent behavior of grease can influence the torque required to rotate a roller.
At low temperatures, grease may become more resistant to movement, increasing rotational drag. At elevated temperatures, the lubricant must still provide adequate film formation and resist deterioration or leakage.
Too little grease can reduce bearing protection, while excessive filling may increase churning losses or create other operational problems depending on the bearing and seal arrangement.
For long mine conveyors, the lubricant should be selected according to:
- Expected operating temperature range.
- Bearing rotational speed.
- Radial and axial loading.
- Seal design and grease retention.
- Water and dust exposure.
- Required bearing life.
- Compatibility with bearing and seal materials.
A low-friction grease should not be selected without verifying its lubrication performance under the actual mechanical duty.
8. How Roller Diameter Influences Energy Consumption
Roller diameter is an important variable in low-resistance idler selection.
For a given conveyor belt speed, a larger roller diameter results in a lower rotational speed.
n = (60 × v) / (π × D)
n: Roller rotational speed (rpm); v: Belt speed (m/s); D: Roller diameter (m).
For example, at a belt speed of 4 m/s, a roller with a diameter of 133 mm rotates at approximately 574 rpm, while a 159 mm roller rotates at approximately 480 rpm.
The lower rotational speed can influence bearing and seal losses. A larger roller radius may also reduce the equivalent tangential resistance force for a given resisting torque.
A larger diameter can additionally affect belt indentation rolling resistance by changing the contact geometry between the roller and the belt cover.
However, the overall result depends on the complete design. Larger rollers may increase shell weight, material cost, rotating inertia, structural dimensions, and installation requirements.
Therefore, larger diameter should be evaluated as an engineering option rather than treated as an automatic energy-saving guarantee.
Selection principle: Larger idler rollers may reduce rotating and indentation losses in suitable applications, but the final benefit depends on bearing and seal design, belt properties, load, speed, and the resulting roller population. Compare complete roller assemblies rather than diameter alone.
9. Comparing 133 mm, 159 mm and 194 mm Rollers
For a long overland conveyor, several roller diameters may be technically feasible. The most suitable diameter depends on load, speed, structure, maintenance requirements, and total cost.
| Parameter | 133 mm Roller | 159 mm Roller | 194 mm Roller |
| Approximate Speed at 4 m/s | 574 rpm | 480 rpm | 394 rpm |
| Rotational Speed | Higher | Intermediate | Lower |
| Potential Energy Benefit | Depends on complete design | Potential reduction in speed-related losses | Potential further reduction in selected losses |
| Main Trade-Off | Higher rotational speed | Balance of size and performance | Greater dimensions, weight and possible cost |
| Required Verification | Bearing speed and load | Rotational resistance and compatibility | System resistance, load and structural fit |
The table compares rotational speed and general design considerations. It does not establish an actual resistance ranking between three specific commercial rollers.
A well-engineered 133 mm roller may perform better than a poorly designed larger roller. Verified test data are required for a meaningful comparison.
10. Select Carrying and Return Idlers Separately
Carrying and return rollers operate under different mechanical conditions.
Carrying Idlers
Carrying idlers support both the belt and the conveyed material. Their loads depend on bulk density, material cross-section, belt width, idler spacing, and the distribution of weight across the rollers.
They may experience relatively high radial loads, particularly at high-capacity mining conveyor sections.
Return Idlers
Return idlers generally support the empty conveyor belt, although their loading can change because of belt tension, idler configuration, contamination, and other operating effects.
Their individual loads may be lower than those of heavily loaded carrying rollers. However, return rollers can experience significant exposure to belt carryback, moisture, and abrasive particles.
| Selection Factor | Carrying Idlers | Return Idlers |
| Primary Load | Belt and conveyed material | Primarily the returning belt |
| Key Efficiency Concern | Loaded rotational and indentation resistance | Rotational resistance and return-side contact losses |
| Environmental Concern | Dust, loading effects, water and vibration | Carryback, moisture and buildup |
| Main Procurement Requirement | Low resistance with verified load capacity | Low resistance with reliable sealing and cleanliness |
The complete project may benefit from different bearing, seal, and diameter choices for carrying and return applications rather than using one roller specification throughout the conveyor.
11. Why Idler Spacing Affects Total Energy Consumption
Idler spacing directly affects the number of rollers installed along a conveyor. Wider spacing can reduce the number of rotating components, but it also changes the mechanical loading and belt support conditions.
Increasing carrying-idler spacing generally increases the length of belt and material supported by each idler set, assuming other factors remain unchanged.
This can increase individual roller loading and belt sag. The resulting changes may influence indentation resistance, belt flexure, material movement, bearing loads, and fatigue life.
Therefore, fewer rollers do not automatically produce a proportionate reduction in total conveyor resistance.
A suitable spacing design should consider the entire resistance model, acceptable sag, material capacity, belt construction, roller load ratings, and structural requirements.
For more information, see Conveyor Idler Spacing: How to Select the Right Distance.
12. Select Shaft Diameter and Shell Strength for Real Operating Loads
Low rotational resistance does not eliminate the structural requirements of a heavy-duty conveyor roller.
The shaft must support the applied loads while maintaining suitable bearing alignment. The shell must resist deformation and support the belt under normal and maximum operating conditions.
An undersized shaft may deflect excessively, altering the operating alignment of the bearings. This can increase internal loading, resistance, and the risk of premature failure.
Likewise, inadequate shell stiffness can lead to deformation under heavy material loading, affecting belt contact and the roller’s long-term reliability.
When comparing low-resistance rollers, verify:
- Maximum radial and applicable axial loads.
- Roller shaft diameter and material grade.
- Shell diameter, wall thickness and construction.
- Bearing-center distance.
- Shaft deflection under load.
- Shell deformation and load capacity.
- Operating speed and fatigue requirements.
A roller should not be made structurally weaker simply to reduce rotating mass or initial cost.
13. Does a Lightweight HDPE Roller Always Have Lower Resistance?
HDPE and other engineered polymer rollers are sometimes considered for applications where low shell weight, corrosion resistance, and operating noise are important.
Reducing roller mass can lower rotational inertia, which may be useful during acceleration and deceleration. However, rotational inertia is not the same as steady-state rotational resistance.
A lightweight roller still requires bearings, seals, a shaft, and a mechanically suitable shell construction. These components determine much of its operating resistance and durability.
For heavy-duty mining conveyors, HDPE or composite roller suitability must also be checked against load capacity, shell deformation, operating temperature, UV exposure, creep behavior, and long-term structural performance.
| Roller Construction | Potential Advantage | Required Verification |
| Steel Roller | High stiffness and established heavy-duty construction | Bearing and seal resistance, mass, corrosion protection |
| HDPE Roller | Low shell mass and resistance to metallic shell corrosion | Deformation, load capacity, temperature, bearing design |
| Composite Roller | Potential balance of mass and mechanical performance | Verified stiffness, fatigue, sealing and operating resistance |
Material type should be considered alongside verified resistance testing and mechanical performance, rather than used as a substitute for those measurements.
14. Temperature Can Change Idler Resistance Significantly
Many long mine conveyors operate outdoors, where the temperature can vary substantially between seasons and between day and night.
Temperature affects bearing lubrication, seal behavior, material expansion, and the mechanical properties of the conveyor belt cover.
At low temperatures, grease resistance can increase. This may raise the rotational resistance of bearings and grease-filled labyrinth seals.
Cold weather can also increase belt indentation rolling resistance depending on the rubber formulation and operating conditions.
At high temperatures, bearing lubrication and the long-term performance of seals and polymer components must remain suitable for the expected service conditions.
For mines in cold regions, specifying idler resistance at room temperature alone may underestimate the resistance experienced during winter startup and operation.
Request resistance data or engineering verification over the relevant temperature range, particularly where the conveyor operates continuously in extreme conditions.
15. Manufacturing Accuracy Supports Consistent Low Resistance
Low rotational resistance depends not only on component selection but also on manufacturing and assembly quality.
Two rollers using similar bearings and seals can perform differently because of variations in machining accuracy, housing alignment, shaft geometry, assembly tolerances, and lubrication.
Important manufacturing checks include:
- Shaft straightness and dimensional accuracy.
- Bearing housing concentricity.
- Correct bearing fits and installation.
- Shell roundness and radial runout.
- Seal geometry and assembly condition.
- Lubricant specification and filling control.
- Axial clearance where relevant.
- Rotational resistance consistency across production samples.
For a large mine project, repeatability may be as important as the best individual laboratory result. The supplier should demonstrate that the production process can maintain the agreed performance and dimensional requirements.
16. Estimate Potential Energy Savings from Lower Idler Resistance
The energy-saving value of low-resistance idlers becomes easier to evaluate when the measured reduction in resistance is converted into mechanical power.
For a simplified conveyor operating at constant belt speed:
ΔP = N × ΔF × v
ΔP: Reduction in mechanical power (W); N: Number of individual rollers; ΔF: Average equivalent tangential resistance reduction per roller (N); v: Belt speed (m/s).
Consider an illustrative long-distance mine conveyor with the following assumptions:
- 6000 individual rollers are being considered for replacement.
- The current rollers have an average equivalent rotational resistance of 4.0 N.
- The proposed rollers have an average equivalent rotational resistance of 2.5 N.
- The belt operates at 4 m/s.
- The conveyor operates for 6500 hours per year.
| Calculation | Illustrative Result |
| Resistance Reduction per Roller | 1.5 N |
| Total Resistance Reduction | 9000 N |
| Mechanical Power Reduction | 36 kW |
| Annual Mechanical Energy Reduction | 234,000 kWh |
In this simplified example, reducing the average rotational resistance by 1.5 N per roller produces an estimated 36 kW reduction in mechanical power demand at the selected belt speed.
Over 6500 operating hours, this corresponds to 234,000 kWh of mechanical energy. The corresponding electrical energy saving would depend on drive efficiency, operating conditions, and whether the conveyor is motoring or regenerating power.
Calculation limitation: These values are illustrative, not measured savings for a specific conveyor or product. They assume the resistance reduction applies across all 6000 rollers at the stated operating condition, with other conveyor losses remaining unchanged. Actual annual savings require load-dependent measurements, operating profiles, installed roller counts, and a complete conveyor energy assessment.
17. Calculate Lifecycle Cost, Not Only Purchase Price
Low-resistance idlers may cost more than conventional roller assemblies because of bearing quality, sealing design, dimensional controls, or specialized construction.
The higher purchase price may be justified when verified energy savings and maintenance benefits exceed the additional investment.
A lifecycle comparison should include:
- Initial roller purchase cost.
- Transportation and installation cost.
- Expected energy consumption.
- Operating hours and electricity price.
- Expected bearing and seal life.
- Inspection and replacement labour.
- Equipment availability and downtime consequences.
- Spare-part inventory and standardization.
- Future maintenance and replacement costs.
Where the measured energy saving is reliable, a preliminary simple payback calculation can compare the incremental project cost with the expected annual net savings.
Simple Payback = Additional Investment / Annual Net Savings
Annual net savings should account for energy benefits and any supported differences in maintenance and operating cost.
A higher-priced idler is not necessarily the most economical option. The best purchase decision should compare validated performance and expected service life under the actual mine conditions.
18. Avoid Sacrificing Sealing and Durability for Low Initial Drag
Mining conveyors frequently operate in demanding environments containing dust, abrasive material, rainfall, washdown water, and temperature changes.
A laboratory comparison may identify a low-drag sealing arrangement, but its field performance also depends on contamination protection and mechanical durability.
If contaminants reach the bearing, rotational resistance can rise as wear develops. The roller may eventually become noisy, difficult to rotate, or seized.
A seized roller can create severe belt contact damage and additional resistance, potentially causing maintenance costs much greater than the original idler price difference.
Low-resistance idlers should therefore be evaluated for both initial and sustained performance.
For heavy-duty applications, request evidence of suitable dust and water protection, bearing life, and resistance consistency where available.
19. Consider Belt Alignment and Installation Accuracy
Correct installation supports efficient idler operation.
When idler frames are misaligned, the rollers may contact the belt at unintended angles. This can introduce additional sliding, uneven loading, belt tracking problems, and increased wear.
Consequently, even a roller with low laboratory rotational resistance may not deliver the expected system benefit when installed in a poorly aligned conveyor structure.
For long overland conveyors, idler frame alignment, roller orientation, structural straightness, and belt loading position should be checked during installation and maintenance.
Special arrangements, including banked idlers for horizontal curves, should follow their approved engineering geometry rather than being aligned using generic straight-conveyor assumptions.
For related design considerations, see Horizontal Curve Idlers for Mine Overland Conveyors.
20. Evaluate the Belt Bottom Cover Alongside Idler Resistance
The bottom cover of the conveyor belt plays an important role in indentation rolling resistance.
As the belt passes over the rollers, the rubber cover deforms under contact pressure. The energy lost during repeated deformation depends on the cover compound and the operating conditions.
Some long-distance conveyors use specialized low-indentation-resistance belt compounds as part of an energy-efficiency strategy.
Such belts should be assessed with the selected idler diameter, load, operating speed, and temperature range.
The combination of a suitable low-resistance roller and a properly selected belt bottom cover may provide greater energy savings than optimizing the roller alone.
However, the two benefits should not be added without a consistent conveyor resistance model. Changes in roller diameter, loading, or idler spacing can alter the interactions between individual resistance components.
21. Special Considerations for Downhill and Regenerative Conveyors
Some long-distance mine conveyors transport material downhill and operate in regenerative mode during certain loading conditions.
When gravity supplies more mechanical energy than the conveyor needs to overcome its resistance, the drive system may absorb energy and convert part of it into electrical power.
Reducing idler rotational resistance on such a conveyor does not necessarily reduce measured electrical consumption in the same way as on a conventional motoring conveyor.
Under regenerative operating conditions, lower mechanical losses may increase the energy available for regeneration, subject to the installed electrical drive, operating constraints, and braking system.
The economic benefit therefore depends on the conveyor’s actual power-flow conditions, energy recovery system, and permitted operating modes.
For conveyors that alternate between motoring and regenerative operation, the energy assessment should consider the operating hours and loads in each mode.
22. Testing and Quality Requirements for Low-Resistance Idlers
Buyers should request measurable performance requirements instead of accepting a general marketing description such as energy-saving roller or ultra-low-friction idler.
Depending on the project, applicable roller testing may refer to DIN 22112, specified customer procedures, or other recognized methods for evaluating idler characteristics.
The precise test edition, procedure, operating conditions, and acceptance criteria should be agreed before production because different methods may not produce directly comparable results.
| Test or Inspection | Purpose | Important Requirement |
| Rotational Resistance Test | Measure resistance under defined conditions | Speed, radial load, temperature and method |
| Bearing Load Verification | Confirm operating capacity and life requirements | Calculated radial and axial loads |
| Dust and Water Protection Test | Evaluate sealing effectiveness | Defined exposure and acceptance method |
| Radial Runout Inspection | Verify roller dimensional accuracy | Specified runout limits |
| Axial Displacement Check | Confirm assembly geometry | Approved design tolerance |
| Dynamic Balance Check | Evaluate rotational balance where required | Specified method and acceptance grade |
| Dimensional Inspection | Verify installation compatibility | Roller length, diameter, shaft ends and fits |
| Production Sampling | Check consistency across manufacturing batches | Agreed sample size and acceptance criteria |
For large projects, resistance measurements should be reported using consistent units. If one supplier quotes N·m and another quotes N, convert them using the corresponding roller radius before comparing the results.
23. What Information Should Be Included in the RFQ?
An accurate request for quotation should provide the operating conditions needed to evaluate both energy efficiency and mechanical reliability.
| RFQ Category | Required Information |
| Conveyor Details | Conveyor length, route profile, belt width, belt speed and operating hours |
| Material Characteristics | Material type, capacity, bulk density, particle size and abrasiveness |
| Idler Arrangement | Carrying or return duty, number of rollers, trough angle and spacing |
| Roller Dimensions | Diameter, shell length, wall thickness, shaft size and mounting ends |
| Operating Loads | Normal and maximum radial loads, relevant axial loads, impact conditions |
| Resistance Requirements | Maximum allowable rotational resistance, test speed, load and temperature |
| Bearing Requirements | Bearing type, model, internal clearance, life and load requirements |
| Sealing and Lubrication | Seal construction, grease requirements, dust and water protection |
| Environmental Conditions | Minimum and maximum temperature, moisture, corrosion and dust exposure |
| Quality Requirements | Test procedures, runout, balance, sampling, inspection records |
| Commercial Information | Quantity by roller type, unit identification, delivery date and destination |
The RFQ should also clarify whether the supplier is responsible only for manufacturing rollers to an approved specification or for providing performance data that supports the conveyor’s energy model.
24. Practical Low-Resistance Idler Selection Checklist
01. Confirm the conveyor length, belt speed and annual operating hours.
02. Determine the number of individual carrying and return rollers.
03. Calculate normal and maximum roller loads for each conveyor section.
04. Request measured rotational resistance at representative loads and speeds.
05. Compare bearing design, quality, clearance and load capacity.
06. Evaluate seal drag together with dust and water protection.
07. Verify lubricant suitability across the operating temperature range.
08. Compare roller diameter options using the complete resistance model.
09. Check shaft strength, shell stiffness and bearing alignment.
10. Verify idler spacing and belt sag requirements.
11. Consider carrying and return idlers separately.
12. Review the influence of the conveyor belt bottom cover.
13. Estimate energy savings from verified resistance differences.
14. Compare lifecycle cost, reliability and maintenance requirements.
15. Agree on testing and inspection acceptance criteria before manufacturing.
16. Verify installation alignment and monitor field performance after commissioning.
25. Common Mistakes When Buying Low-Resistance Idlers
Mistake 1: Choosing Rollers Based on Free-Spinning Time
Hand-spinning tests do not represent the resistance experienced under actual operating load. Controlled resistance testing provides a more reliable comparison.
Mistake 2: Assuming Lightweight Rollers Always Consume Less Energy
Lower mass reduces rotational inertia but does not automatically reduce steady-state bearing and seal resistance.
Mistake 3: Selecting the Lowest-Drag Seal Without Considering Dust
An inadequate seal may allow contamination to increase bearing friction and shorten roller life. Protection and drag must be balanced.
Mistake 4: Ignoring Roller Load During Resistance Testing
Resistance measured without loading may not predict behavior under high material loads or relevant axial forces.
Mistake 5: Comparing Test Values from Different Conditions
Results obtained at different speeds, loads, temperatures, or using different measurement methods may not be directly comparable.
Mistake 6: Assuming Larger Rollers Always Provide Greater Savings
Larger diameter may reduce selected losses, but the result depends on bearing and seal design, belt characteristics, installation cost, and operating conditions.
Mistake 7: Reducing Idler Quantity Without Checking Belt Sag
Wider spacing increases the loading of individual idler sets and can change belt flexure, indentation resistance, and material behavior.
Mistake 8: Ignoring Production Consistency
A single excellent test sample does not guarantee that thousands of production rollers will maintain the same resistance and mechanical quality.
Mistake 9: Treating Idler Resistance as Total Conveyor Resistance
Belt indentation, flexure, material movement, and other losses also contribute to energy consumption. Complete conveyor analysis remains necessary.
Mistake 10: Focusing Only on Purchase Price
Energy consumption, maintenance frequency, bearing failures, downtime, and replacement costs should be included in the economic comparison.
How to Compare Suppliers of Low-Resistance Mining Idlers
For long mine conveyor projects, selecting the right supplier is as important as selecting the roller design.
A suitable supplier should be able to provide clear dimensional specifications, bearing and seal information, mechanical load ratings, and agreed inspection requirements.
Where energy performance is part of the purchasing decision, request comparable rotational resistance test data with the associated loading, speed, temperature, and test method clearly identified.
For large quantities, manufacturing consistency and quality-control procedures deserve particular attention. Variations in bearing fits, shaft geometry, housing alignment, and lubrication can affect the resistance and durability of individual rollers.
The supplier should also be able to manufacture according to approved roller dimensions, shaft-end details, bearing specifications, and frame interfaces.
If replacing existing rollers, confirm whether the proposed low-resistance assembly is interchangeable with the installed frames and suitable for the existing belt speed and loading conditions.
For a broader selection reference, see How to Choose Idlers for Heavy-Duty Belt Conveyors.
Custom Heavy-Duty Conveyor Idlers from SHENGYUAN
SHENGYUAN manufactures conveyor rollers, idlers, frames, pulleys, and related components for mining, quarrying, coal handling, cement plants, ports, power stations, steel plants, and other heavy-duty bulk-material handling applications.
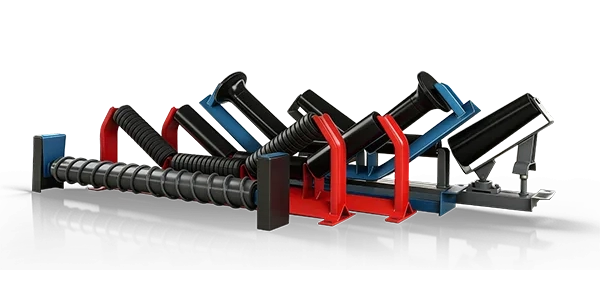
The SWCONS conveyor roller range includes carrying rollers, return rollers, impact rollers, steel rollers, HDPE rollers, spiral return rollers, and other application-specific configurations.
For long-distance mine conveyors, roller specifications can be reviewed according to belt width, speed, expected loading, roller diameter, shell construction, shaft dimensions, bearing type, seal design, operating environment, and required inspection criteria.
Low-resistance performance requirements can be incorporated into the purchasing specification where suitable test methods, operating conditions, and acceptance criteria are agreed. Any energy-saving claim should be supported by relevant measurements and conveyor calculations rather than assumed from the roller’s construction alone.
Through custom conveyor solutions, roller and idler-frame manufacturing can be coordinated with customer drawings, specified materials, bearing and sealing requirements, and installation interfaces.
For large-scale mine conveyor projects, standardized dimensions, consistent manufacturing processes, and clear inspection requirements can help support reliable installation and long-term maintenance.
Need low-resistance idlers for a long-distance mining conveyor?
Send the conveyor length, belt width and speed, material capacity, operating hours, required carrying and return idler arrangements, roller diameter and length, shaft dimensions, bearing and sealing preferences, radial load requirements, temperature range, environmental conditions, and any rotational resistance test specifications. Existing roller performance records, installation drawings, and required quantities can also help establish a suitable technical and commercial quotation.
Conclusion: Select Low-Resistance Idlers Using Verified Performance
Low-resistance idlers can contribute to improved energy efficiency on long mine conveyors, particularly where many thousands of rollers operate continuously.
However, energy performance cannot be evaluated from roller weight, diameter, bearing brand, or free-spinning time alone.
A reliable selection process begins with representative rotational resistance measurements and an understanding of the actual operating loads, belt speed, temperature, and environmental conditions.
Bearing design, seal protection, lubrication, roller diameter, shaft strength, shell stiffness, and manufacturing accuracy must be considered together. Carrying and return idlers may require different specifications, and the interaction between idler resistance and belt indentation rolling resistance should be evaluated in the complete conveyor energy model.
The economic decision should compare verified energy savings with equipment cost, expected service life, maintenance requirements, and the risks associated with dust, water, and mechanical failure.
The best low-resistance idler for a long mine conveyor is not simply the roller with the lowest laboratory drag or the lightest shell. It is a mechanically reliable, well-sealed, accurately manufactured roller whose verified resistance and operating life provide measurable value across the complete conveyor system.