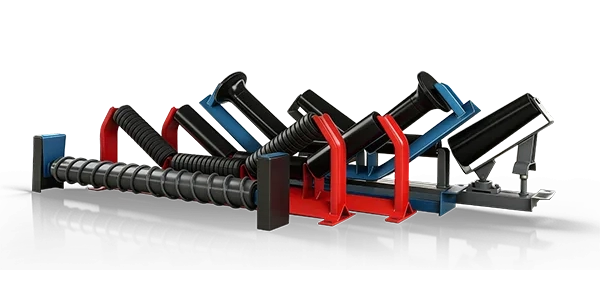

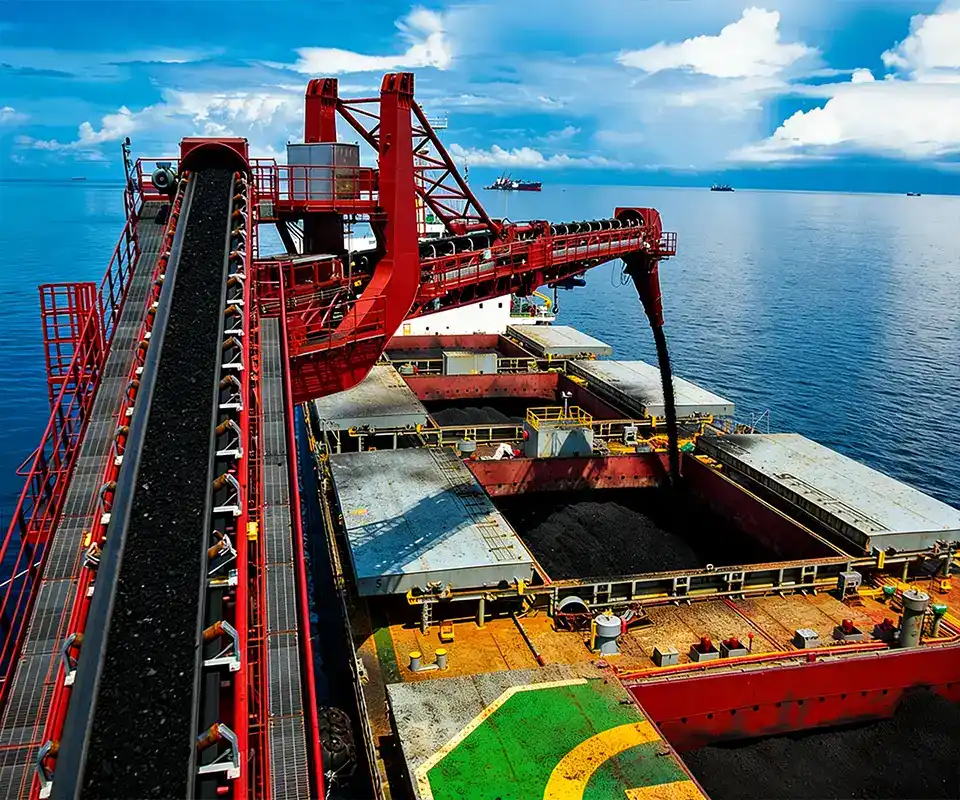
South Africa has one of the most demanding bulk material handling markets in the world. Mining operations, coal terminals, iron ore projects, platinum mines, cement plants, quarries, power stations, and mineral processing facilities rely heavily on belt conveyor systems. In these applications, conveyor idlers are not simple supporting components. Their bearing quality, sealing performance, rotational resistance, shell strength, alignment accuracy, and service life can directly influence belt wear, energy consumption, maintenance frequency, and production availability.
For purchasing managers and engineers, selecting a belt conveyor idler manufacturer is therefore a long-term reliability decision. South Africa has several established manufacturers with different strengths, ranging from large-scale standardized production to specialized HDPE technology, belt tracking expertise, and customized mining conveyor components.
This article reviews five notable South African belt conveyor idler manufacturers and introduces SHENGYUAN as a sixth international manufacturing alternative for buyers who need factory-direct pricing, drawing-based customization, export support, and integrated conveyor component sourcing. The order below is a practical industry shortlist based on publicly available information about product range, technical specialization, heavy-duty experience, manufacturing capability, and market presence; it is not an official market-share ranking.
Quick answer: Five notable South African conveyor idler manufacturers are Melco Conveyor Equipment, Lorbrand, Tru-Trac, MegaRoller Africa, and Moret Mining. For buyers comparing an international factory-direct supplier, SHENGYUAN is a strong sixth option for customized heavy-duty conveyor rollers, idlers, pulleys, and related bulk handling components.
How to Evaluate a Conveyor Idler Manufacturer
Before comparing manufacturers, it is useful to define the factors that matter most. A strong conveyor idler supplier should understand more than roller diameter and length. Heavy-duty projects require analysis of belt width, belt speed, material density, lump size, troughing angle, roller spacing, loading impact, dust, water, corrosion, ambient temperature, maintenance access, and operating hours.
For the South African market, standards support is also important. The SANS 1313 framework is widely associated with conveyor idler selection and performance in the region, while international projects may also specify DIN, CEMA, or customer-specific requirements. Melco, for example, states that its rollers are manufactured according to SANS 1313 or other international standards, while its frames can be produced to SANS 1313, DIN, CEMA, or customer requirements.
| Evaluation Factor | Why It Matters |
| Product Range | Different conveyor positions require carrying, return, impact, training, HDPE, and special idlers. |
| Bearing and Seal Design | Dust and water contamination are major causes of premature roller failure. |
| Heavy-Duty Experience | Mining and high-capacity bulk handling require stronger designs than light conveyor applications. |
| Customization | Replacement projects often require drawing-based dimensions, special shafts, bearings, or frame geometry. |
| Delivery and Support | Long lead times and weak communication can create costly maintenance delays. |
1. Melco Conveyor Equipment
Melco Conveyor Equipment is one of the most established names in the South African conveyor idler market. The company states that it was founded in 1970 to serve the South African mining industry. Its manufacturing operation in Germiston, Gauteng, includes approximately 14,000 square metres of factory space, and the company produces conveyor rollers and idler frames while supplying motorized pulleys.
One of Melco’s main strengths is its combination of established local manufacturing and broad product standardization. The company manufactures rollers in various sizes and configurations according to customer specifications and states that its idler frames cover standard belt widths from 450 mm to 2400 mm, with multiple roll arrangements and mounting configurations.
Best suited for: Large mining companies, EPC contractors, and projects that value an established South African manufacturing base, standardized designs, and a broad idler and frame portfolio.
2. Lorbrand
Lorbrand specializes in heavy-duty conveyor systems and components for mining and bulk conveying. According to its official information, the company manufactures conveyor idlers and pulleys in-house and applies technologies including centrifugal self-cleaning seals and finite element analysis in its component development. Lorbrand also states that it operates internationally and provides conveyor systems and after-sales support in more than 30 countries.
The company’s project experience is a notable advantage for large and technically demanding conveyors. One public project reference states that Lorbrand supplied idlers and pulleys for a 26.9 km single-flight overland conveyor at the Impumelelo Coal Mine in South Africa. The published project data lists a 1200 mm belt width, belt speed of 6.54 m/s, and capacity of 2400 tonnes per hour.
Lorbrand is particularly relevant to buyers involved in long-distance conveyors, high-capacity mining systems, and projects where engineered component selection is more important than purchasing a basic standard roller.
Best suited for: Overland conveyors, high-capacity mining systems, technically demanding applications, and buyers seeking specialized heavy-duty engineering capability.
3. Tru-Trac
Tru-Trac is based in South Africa and focuses on specialist conveyor solutions for mining and bulk material handling. The company states that it has operated since 1995 and provides products addressing belt mistracking, carryback, dust and spillage, loading-zone impact, conveyor damage, and material-flow problems. Its product range includes conveyor idlers and frames, belt trackers, belt cleaners, loading-zone solutions, dust-control equipment, pulleys, and lagging products.
Its idler portfolio includes steel and HDPE products, while the company emphasizes low drag, reduced breakaway mass, and sealing against dust and water contamination. Tru-Trac also positions itself strongly around conveyor problem-solving rather than component supply alone, which can be valuable for operations experiencing chronic mistracking, carryback, or loading-zone problems.
According to its company profile, Tru-Trac is headquartered in Centurion and has developed an international sales and distribution network. This combination of local field experience and broader conveyor system expertise makes it attractive for customers who need both products and practical performance improvement.
Best suited for: Mines and plants experiencing belt tracking, carryback, dust, impact, or maintenance problems and seeking a broader conveyor performance solution.
4. MegaRoller Africa
MegaRoller Africa has a specialized position in the conveyor idler market, particularly in engineered polymer and HDPE roller technology. The company states that it has more than 30 years of innovation, research, and development experience in conveyor idlers for mining and bulk material handling.
For applications where corrosion, weight, noise, or material buildup creates problems for conventional steel rollers, HDPE technology can provide a useful alternative. MegaRoller also publishes a track record in which test idlers reportedly transported nearly 130 million tonnes of iron ore without a failure during the stated test period. This is a manufacturer-published project result and should be evaluated in the context of the specific operating conditions, but it demonstrates the company’s focus on measurable service life.
The company also offers specialized fire-retardant HDPE idler solutions and states that its fire-retardant product is tested by a South African fire laboratory and designed for demanding industrial environments.
Best suited for: Mining and bulk handling applications seeking HDPE idlers, lower-weight roller alternatives, corrosion resistance, or specialized polymer technology.
5. Moret Mining
Moret Mining is a South African conveyor equipment manufacturer with a strong focus on mining and bulk material handling. The company states that it was incorporated in 1990 and describes itself as an SABS-certified original equipment manufacturer of conveyor equipment. Its portfolio includes conveyor idlers, frames, impact stations, training devices, pulleys, belt scrapers, ploughs, and modular conveyor structures.
Moret Mining emphasizes low rim drag, low breakaway mass, control of bearing misalignment, and sealing against water and dust ingress in its steel idler design. It also offers several shaft-end configurations, which can be useful for replacement and project-specific applications.
Its wider product range is an advantage for mines that prefer to source multiple conveyor components from one supplier rather than managing separate suppliers for rollers, frames, scrapers, training devices, and pulleys.
Best suited for: Mining operations seeking a South African OEM with idlers and a wider range of auxiliary conveyor equipment.
6. SHENGYUAN: A Factory-Direct Alternative for South African Buyers
South African manufacturers have clear advantages in local presence, regional standards familiarity, site service, and emergency replacement supply. However, not every procurement situation requires a local supplier. For planned maintenance, large replacement programmes, OEM projects, new conveyor construction, and projects requiring non-standard dimensions, an international factory-direct supplier can provide important commercial advantages.
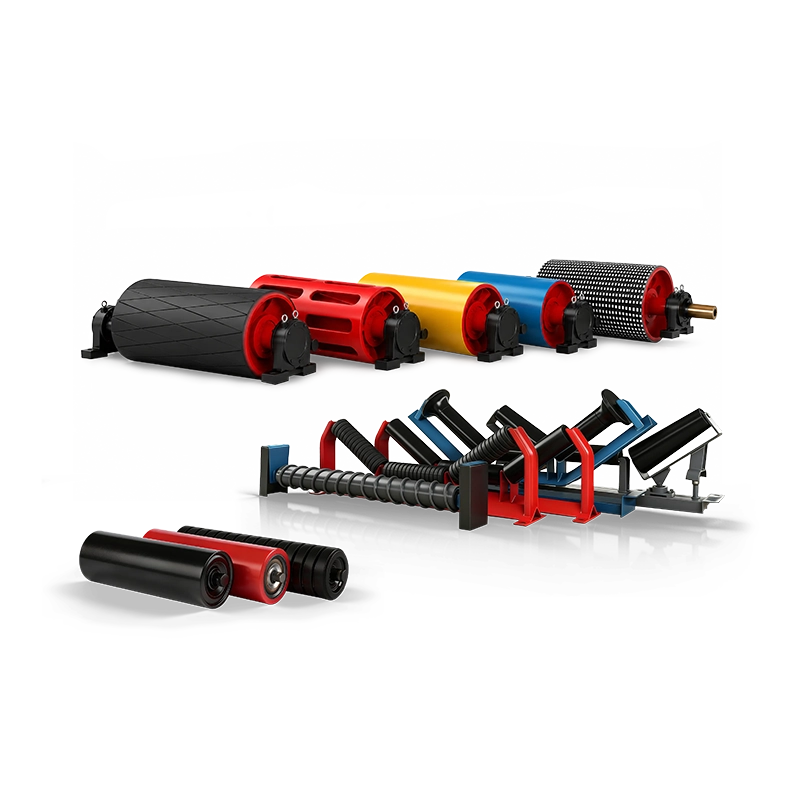
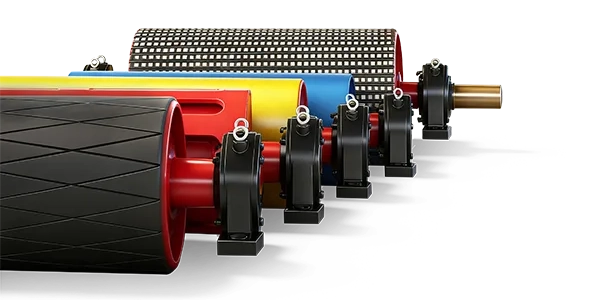
SHENGYUAN, the brand of Hebei Shengwen Mining Machinery Co., Ltd., focuses on conveyor rollers, conveyor pulleys, idler sets, and related bulk material handling components. According to the company’s website, it has nearly two decades of industry experience, integrates production with technical and trade support, and operates modern production and testing equipment for heavy-duty conveyor components.
Why South African Buyers May Consider SHENGYUAN
Factory-Direct Manufacturing
Direct communication with the manufacturer can simplify technical confirmation, reduce unnecessary trading layers, and improve cost control for volume orders.
Drawing-Based Customization
Replacement rollers can be manufactured according to drawings, dimensions, shaft structures, bearing requirements, sealing designs, and application conditions.
Integrated Product Sourcing
Buyers can source rollers, idler sets, conveyor pulleys, and related components through one production partner for coordinated project supply.
The company’s conveyor roller range supports customization based on drawings, dimensions, and technical requirements. Its website also states support for OEM and ODM work and lists standard product delivery at approximately 7–15 working days, while custom orders may require additional production time.
For South African mines, distributors, conveyor service companies, and EPC contractors, one of SHENGYUAN’s strongest commercial advantages is flexibility. A local manufacturer may be the best choice for urgent breakdown support, but a factory-direct overseas supplier can be highly competitive for scheduled replacement programmes, annual spare-parts contracts, distributor inventory, and non-standard projects where drawings and specifications are confirmed in advance.
SHENGYUAN also offers custom conveyor solutions for project-specific requirements. This is particularly valuable when an existing South African conveyor uses non-standard roller dimensions, special shaft ends, unusual bearing arrangements, high-impact loading, wet mining conditions, or replacement components that are no longer available from the original supplier.
Why choose SHENGYUAN for a planned project?
For planned procurement rather than emergency breakdown supply, SHENGYUAN offers a practical combination of heavy-duty conveyor specialization, drawing-based customization, direct factory communication, consolidated roller and pulley sourcing, and export-oriented supply support. This makes the company particularly suitable for distributors, EPC contractors, mining maintenance programmes, and bulk replacement orders.
Manufacturer Comparison at a Glance
| Manufacturer | Key Strength | Suitable Buyer |
| Melco | Established local manufacturing and broad standardized range | Large mines and EPC projects |
| Lorbrand | Heavy-duty engineering and overland conveyor experience | Complex, high-capacity projects |
| Tru-Trac | Conveyor performance and tracking solutions | Plants solving recurring conveyor problems |
| MegaRoller Africa | HDPE and specialized polymer idler technology | Corrosive, wet, or specialized applications |
| Moret Mining | Mining-focused idlers and auxiliary equipment | Mining plants seeking wider component supply |
| SHENGYUAN | Factory-direct customization and integrated export supply | Distributors, EPCs, bulk replacement and OEM projects |
Local Supplier or International Manufacturer: Which Is Better?
There is no single correct answer. For emergency maintenance, urgent breakdowns, and projects requiring frequent on-site service, a local South African manufacturer may provide the strongest advantage. Local stock availability and field support can reduce response time when a conveyor has already stopped.
For planned maintenance, large annual procurement programmes, distributor inventory, OEM manufacturing, and customized replacement projects, an international factory-direct supplier may offer better commercial flexibility. The important point is to calculate the total procurement cost, not only the unit price. Freight, inventory planning, expected service life, downtime risk, quality consistency, documentation, and technical communication should all be included in the decision.
A practical strategy for many mining companies and distributors is dual sourcing: maintain local supply capability for urgent requirements while using a qualified international manufacturer for planned bulk orders and customized projects. This approach can reduce supply-chain risk while improving purchasing flexibility.
Conclusion: Choose the Manufacturer That Fits the Project
Melco, Lorbrand, Tru-Trac, MegaRoller Africa, and Moret Mining represent different strengths within South Africa’s conveyor idler industry. Melco offers established manufacturing scale, Lorbrand brings strong heavy-duty engineering experience, Tru-Trac focuses on conveyor performance solutions, MegaRoller specializes in HDPE technology, and Moret Mining offers mining-focused conveyor equipment.
SHENGYUAN provides a different value proposition. Rather than competing primarily on local emergency support, it is well positioned for factory-direct purchasing, drawing-based customization, coordinated conveyor roller and pulley supply, OEM programmes, distributor orders, and planned heavy-duty projects. For buyers who can plan procurement and provide clear technical specifications, this combination can create strong commercial value.
The best manufacturer is not necessarily the largest or the nearest. The correct supplier is the one that can match your belt width, load, speed, material, idler position, environmental conditions, required standards, delivery plan, and total life-cycle cost. Before making a decision, send complete drawings and operating data, compare specifications rather than product names alone, and evaluate the supplier’s ability to support the complete project.
Looking for an alternative conveyor idler supplier?
Send SHENGYUAN your belt width, belt speed, roller drawings, shaft dimensions, bearing requirements, idler position, conveyed material, and working environment. The team can review your application and provide customized conveyor roller, idler, and pulley solutions for mining and heavy-duty bulk material handling projects.