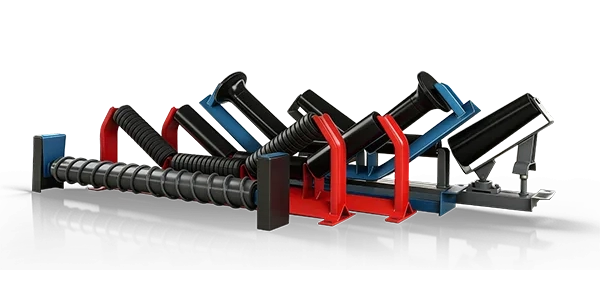

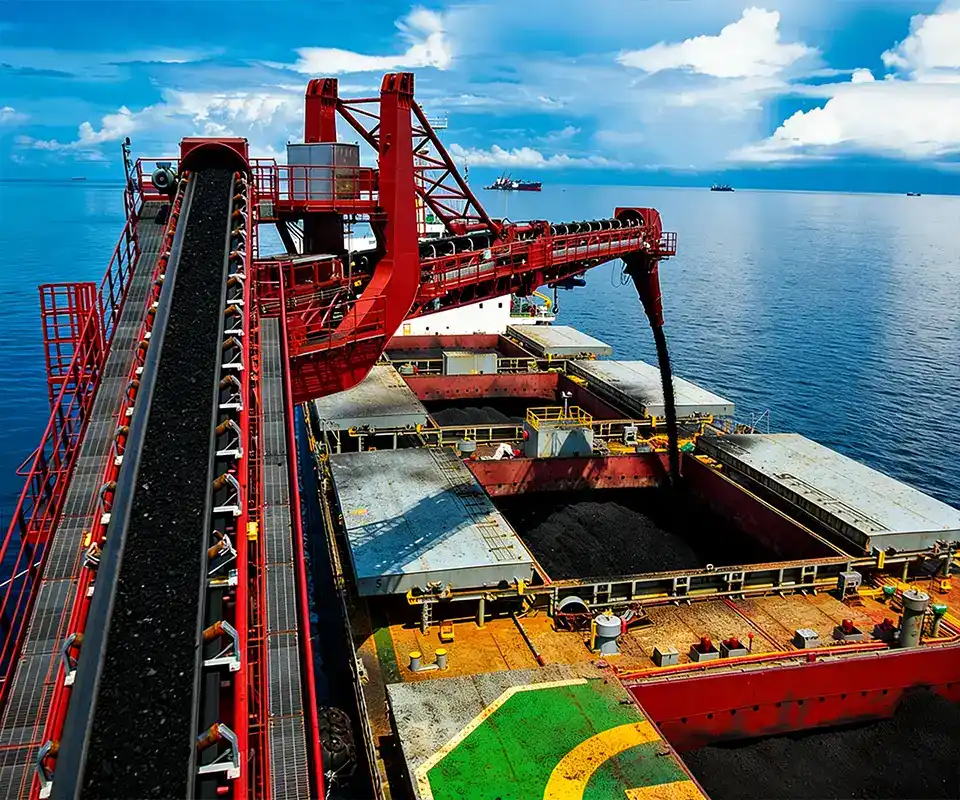
A conveyor belt may have enough theoretical capacity for the required tonnage and still be unsuitable for the largest pieces of material. Oversized or irregular lumps can interfere with skirtboards, become unstable during transfer, or concentrate impact loads on the belt and its supports.
Choosing belt width therefore requires two separate checks: whether the material can be handled reliably and whether the conveyor can deliver the required capacity. Maximum lump size helps identify candidate widths, but it cannot determine the final specification alone.
Quick answer: Measure the largest expected pieces, establish their proportion in the material stream, and use a selection reference appropriate to the conveyor. Then verify capacity, belt speed, loading geometry, and component compatibility. There is no single belt-width-to-lump-size ratio that applies to every bulk material conveyor.
Belt Width and Maximum Lump Size: A Training Reference
The following values reproduce Table 1 on slide 6 of Shengwen’s Belt Conveyor Training material, within its discussion of DTII(A) conveyors. The table defines lump size as the material’s maximum linear dimension. It provides a preliminary reference, not a universal design standard.
| Belt Width | Maximum Lump Size Listed | How to Use the Entry |
| 500 mm | 100 mm | Preliminary candidate within this reference. |
| 650 mm | 150 mm | Confirm material distribution and loading conditions. |
| 800 mm | 200 mm | Check conveying capacity separately. |
| 1000 mm | 300 mm | Review lump shape, loading impact, and clearances. |
| 1200 mm | 350 mm | Final suitability requires application-specific verification. |
| 1400 mm | 350 mm | The repeated value is specific to this table. |
Scope matters: This training table does not state the percentage of large lumps or provide every design assumption. Its values should not be presented as guaranteed handling limits, universal minimum widths, or proof of compliance with a particular standard.
Measure the Largest Pieces, Not Only the Nominal Product Size
Under the definition used in the training table, a rock measuring 260 × 170 × 120 mm has a maximum linear dimension of 260 mm. However, all three dimensions remain useful because a long, flat piece can interact with a chute differently from a compact lump.
A nominal crusher product size or screen opening is not necessarily identical to the longest dimension of every discharged piece. Identify the measurement method and distinguish normal production from occasional oversize caused by bypasses, damaged screens, or process changes.
Collect representative size-distribution information and photographs with a scale using an approved sampling procedure. Never retrieve or measure material by reaching into an operating conveyor.
Use the Table to Identify Candidates, Not Approve a Design
These examples illustrate how to read the training reference. They do not establish that the indicated belt will suit every material with that lump size.
Example: 90 mm Lump
The 500 mm entry is the first listed candidate because its associated lump-size value is 100 mm.
Example: 130 mm Lump
The first matching entry is 650 mm, associated with a listed lump size of 150 mm.
Example: 180 mm Lump
The 800 mm entry becomes a candidate for further checking against capacity and material behavior.
Why Different Selection References Give Different Values
Maximum size does not describe how frequently large pieces occur. A stream containing occasional large lumps among fines differs from one consisting mainly of similarly sized coarse pieces. Shape, loading arrangement, and the material profile on the belt also influence selection.
For example, Table 3 in Rulmeca’s bulk-handling technical information distinguishes uniform and mixed lump sizes when relating material size to belt width and speed. This illustrates why values from different references should not be combined without checking their assumptions.
Specify the reference and its conditions alongside the selected width. A recommendation based only on “the belt should be several times wider than the largest lump” leaves important information unresolved.
What Does the 350 mm Entry Actually Mean?
The training table lists 350 mm for both 1200 and 1400 mm belts. Preserve those values when reproducing the table, but do not interpret them as proof that all 1400 mm conveyors are physically incapable of handling larger pieces.
For material above 350 mm: This particular table no longer provides a selection basis. Obtain an application-specific assessment covering material distribution, belt geometry, loading impact, clearances, and support loads. Do not extrapolate an unsupported value for a wider belt.
Check Capacity After the Lump-Size Review
Mass throughput and volumetric capacity are different quantities. Convert the required tonnes per hour using the material’s loose bulk density, not the density of solid rock. For variable material, a lower bulk density requires more conveying volume for the same tonnage.
Capacity relationship: Required volume in m³/h = throughput in t/h ÷ loose bulk density in t/m³.
Consider a hypothetical crushed-stone application with 180 mm maximum lumps, a peak requirement of 800 t/h, and loose bulk density of 1.5 t/m³. The required conveying volume is approximately 533 m³/h.
The training material’s separate capacity table on slide 10 lists 496 m³/h for an 800 mm belt at 2.0 m/s. Its stated conditions are horizontal conveying, a 20-degree dynamic surcharge angle, and a 35-degree idler trough angle. Under that reference, the 800 mm candidate falls short of the required volume.
The same table lists 811 m³/h for a 1000 mm belt at 2.0 m/s, making it another candidate to investigate. This is not final approval: actual loading, incline, surges, edge clearance, and operating allowance still require review. Our belt width, speed, and capacity guide addresses that broader calculation.
Review Speed and Loading Conditions Together
Increasing speed can raise theoretical capacity, but it does not create additional physical clearance for oversized pieces. It also changes the relationship between the incoming material stream and the receiving belt, as well as discharge trajectories.
Assess drop height, incoming velocity, lump mass, and the risk of pieces rolling or wedging. Guide material toward the conveyor centerline and check the clear opening between chute liners and skirts. Nominal belt width is not the same as usable loading-zone width.
Large-lump applications may require different impact support and belt construction. See when impact idlers are required for the supporting considerations. A wider belt alone cannot correct an unsuitable transfer arrangement.
Check the Existing Conveyor Before Increasing Belt Width
Replacing an 800 mm belt with a 1000 mm belt is not necessarily a belt-only modification. Review pulley face widths, idler geometry, frame clearance, transition distances, cleaners, chutes, and guarding. Recalculate relevant loads and drive requirements if capacity or operating conditions change.
Width also does not specify tensile strength, cover thickness, or resistance to cutting. These are separate selection decisions, even when the proposed width is suitable.
Information Needed for a Belt-Width Recommendation
01. Maximum piece dimensions, measurement method, and expected oversize.
02. Particle-size distribution, lump shape, and photographs with a scale.
03. Normal and peak throughput, loose bulk density, and moisture range.
04. Belt speed, conveyor length, lift, incline, and trough geometry.
05. Loading height, transfer drawings, chute clearances, and impact support.
06. Existing belt specification, component dimensions, and failure history.
Discuss Belt and Component Compatibility with SHENGYUAN
SHENGYUAN supplies conveyor belts alongside rollers, pulleys, and related conveyor components. This supports a purchasing discussion that considers the belt and its interfaces together.
Through its custom solutions service, customers can discuss drawings and project requirements before manufacturing. Ask the proposal to identify selection assumptions, component scope, and any calculations still requiring confirmation.
Start with the material and operating data
Send representative lump measurements, peak throughput, bulk density, and conveyor drawings. These details provide a stronger basis for a recommendation than specifying belt width from one lump-size value alone.
Conclusion
Maximum lump size is an important belt-width constraint, but its meaning depends on the selection method and material conditions. Use reference tables within their stated scope, verify capacity independently, and review transfer geometry and component compatibility. The final width should satisfy the complete application, not merely match one table entry.